Periodic reverse-current electrolysis for copper is a refining method that involves periodically reversing the direction of the current in the electrolytic cell for short intervals; adjusting the current direction prevents anode passivation and boosts production capacity. This method was first employed in electroplating in 1949 to produce smooth, high-quality coatings. Driven by rising copper demand in the 1960s, countries such as Japan, Sweden, Zambia, and China conducted extensive research on the technique and gradually implemented it in copper refineries.
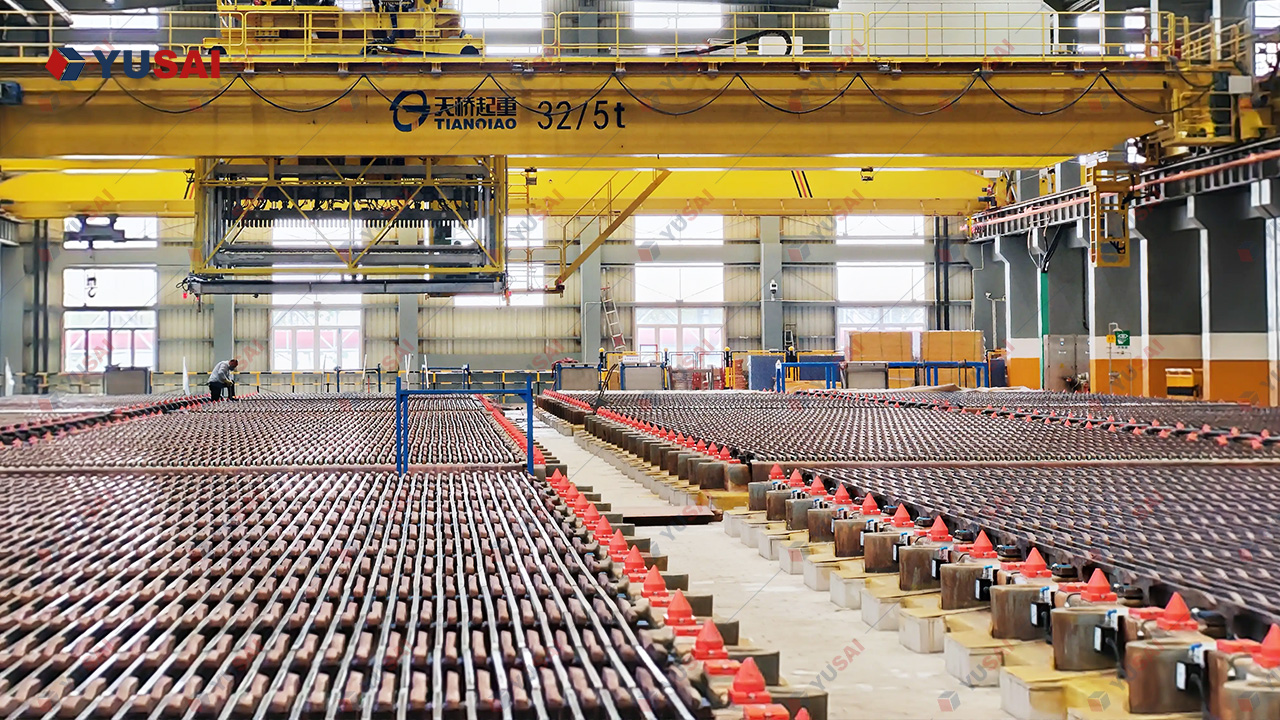
The underlying principle is as follows: during the forward current phase, conventional electrolysis takes place; during the reverse current phase, the anode switches to a cathode, causing copper ions near the electrode to redeposit and reducing the concentration gradient to prevent passivation. Simultaneously, the original cathode becomes an anode, and surface protrusions dissolve, thereby enhancing purity. A typical cycle consists of 100–200 seconds of forward current and 5–10 seconds of reverse current, with a commutation interval of 0.1–0.4 seconds. While this method allows current density to reach 400 A/m² and increases output by 15%, the reversal process reduces current efficiency and raises power consumption. It was not until the advent of high-power thyristor rectifiers and contactless rapid-reversing switches that periodic reverse-current electrolysis was successfully applied in large-scale copper refineries in Japan, Zambia, the United States, and South Africa starting in 1969. Trials of this technology in my country began in 1971 [1]. In 1997, a controlled constant-current system with periodic reversal capabilities—designed for a 100,000-tonne copper electrolysis plant by the Automation Research Institute of the Ministry of Metallurgical Industry and other entities—was put into operation. In 2011, research was conducted on the design and practical implementation of the main circuit and control circuitry for the rectifier power supply used in this process.
A copper electrolytic refining method involving the periodic reversal of current direction in the electrolytic cell for short durations.
First used in electroplating in 1949 to achieve smooth, high-quality coatings, the technology was later adopted for industrial use in copper refineries across Japan, Zambia, the United States, and South Africa in 1969, following the introduction of high-power thyristor rectifiers and contactless rapid-reversing switches. Experimental work on periodic reverse-current electrolysis in my country began in 1971.
Development History
Periodic reverse-current electrolysis technology was first applied to electroplating in 1949, yielding smooth, high-quality coatings on plated parts. However, due to the extremely high frequency of current reversal required, the technology was not applied to industrial electrolysis—specifically at large copper refineries in Japan, Zambia, the United States, and South Africa—until 1969, following the advent of high-power thyristor rectifiers and contactless rapid-reversal switches.
Experimental work on periodic reverse-current electrolysis in my country began in 1971. In 1973, an expanded trial of lead electrolysis was conducted at the (former) Shenyang Smelter using a current intensity of 6,400–7,400 A; the results showed a current efficiency of 92.76%–93.37%, with the resulting electrolytic lead featuring a smooth surface and high quality.
Technological advancements paved the way for large-scale industrial applications; for instance, in May 1997, a periodic reverse-current, thyristor-based constant-current control and monitoring system for a 100,000-ton copper electrolysis plant was put into operation. In the 21st century, research into power supply and control technologies for periodic reverse-current electrolysis has continued; notably, a 2011 study involved the design and practical implementation of the main and control circuits for a rectifier power supply used in periodic reverse-current copper electrolysis.
Principles and Characteristics
During the reverse-current phase, sharp-tipped particles growing on the cathode can be dissolved and removed, thereby preventing short circuits between the electrodes. Frequent current reversal and oscillation mitigate concentration polarization, loosen and detach the thick, hard layer of anode slime from the anode surface, and prevent anode passivation. Although the reverse current represents “non-productive work” in terms of net metal deposition, it enables the production of high-quality electrolytic products.