Overview
Copper anode slime is a high-value secondary raw material generated during copper electrorefining, rich in gold, silver, selenium, tellurium, copper and other valuable metals. Traditional pyrometallurgical routes for copper anode slime treatment suffer from heavy flue gas pollution, long production cycles, high capital investment, poor working conditions and difficulties in comprehensive utilization of multiple valuable elements. This article introduces a full hydrometallurgical technology for selective extraction of gold and silver from copper anode slime. The process uses atmospheric-pressure sulfuric acid decoppering followed by acidic thiourea selective leaching of precious metals, and recovers Au-Ag alloy directly through diaphragm electrowinning.
The technology achieves gold leaching rate >95%, silver leaching rate >99%. The electrowinning deposition rate of gold exceeds 99.5% and silver exceeds 98.5%. The overall direct recovery of gold is above 94% and silver above 96%. It runs under mild temperature and atmospheric pressure, produces no harmful smelting fumes, keeps selenium and tellurium concentrated in leaching residue for separate recovery, and features low operating cost and smaller environmental footprint.
Feed Material Characteristics
This process is suitable for copper anode slime with the following typical composition (mass fraction): Silver: 5%–25% Gold: 0.05%–2.0% Selenium: 3%–10% Tellurium: 0.3%–1.0% Copper:13%–25%
Process Principle & Technical Flow
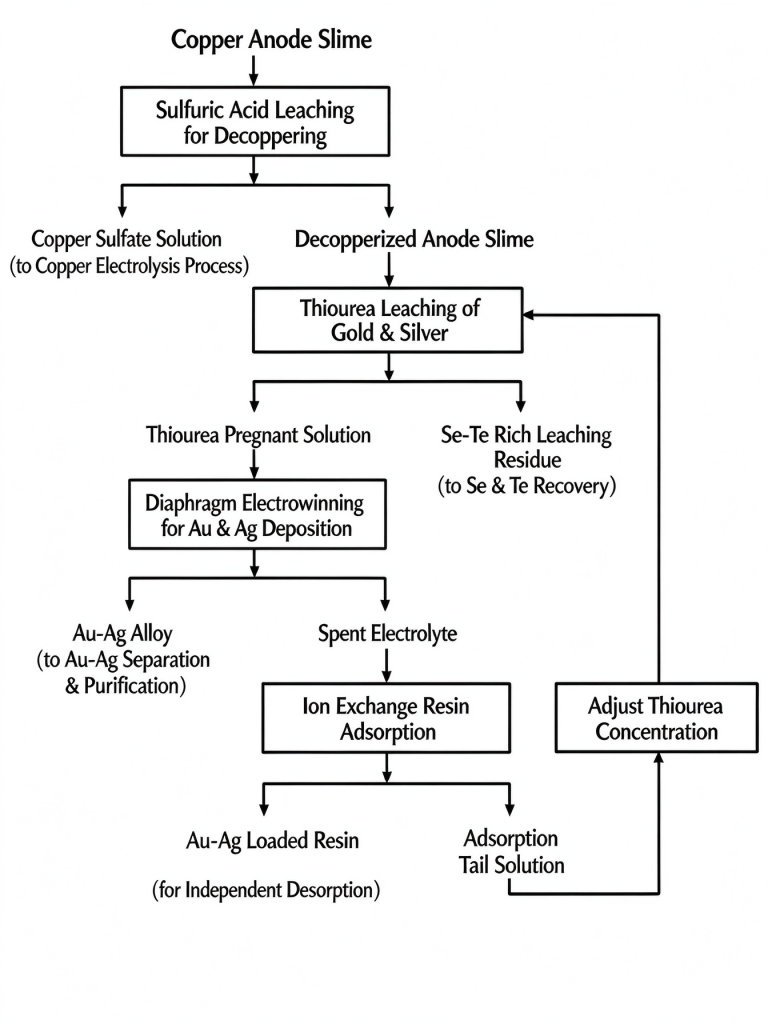
The whole process consists of three core stages: decoppering pretreatment, thiourea selective leaching of gold & silver, and diaphragm electrowinning for Au-Ag alloy deposition.
- Atmospheric Sulfuric Acid Decoppering The raw copper anode slime is milled to 200–300 mesh. Pulp is prepared at liquid-solid ratio 3–5 mL/g with dilute sulfuric acid. Sulfuric acid dosage is 1.2–1.5 times the theoretical stoichiometric amount for copper reaction. Leaching proceeds at ambient temperature with air sparging and stirring for 16–24 hours. Single or multi-stage leaching is applied until residual copper in decopperized anode slime drops below 1%. After filtration and washing, copper sulfate solution is obtained and returned to copper electrorefining workshop; solid cake is decopperized anode slime for next leaching.
- Acidic Thiourea Selective Leaching of Gold and Silver Decopperized anode slime is mixed with thiourea solution at liquid-solid ratio 10–20 mL/g. Thiourea concentration is controlled at 30–70 g/L. Ferric ions and / or hydrogen peroxide are added as oxidants. The slurry pH is adjusted to 0.5–1.5 by sulfuric acid or mixed sulfuric-nitric acid. Leaching temperature is kept between 30–60 ℃ with reaction duration 16–24 hours. Multi-stage leaching is adopted to guarantee gold leaching rate >95% and silver >99%. After solid-liquid separation, the filtrate is thiourea pregnant solution containing gold and silver. The leaching residue is rich in selenium and tellurium, which can be further processed for Se and Te recovery.
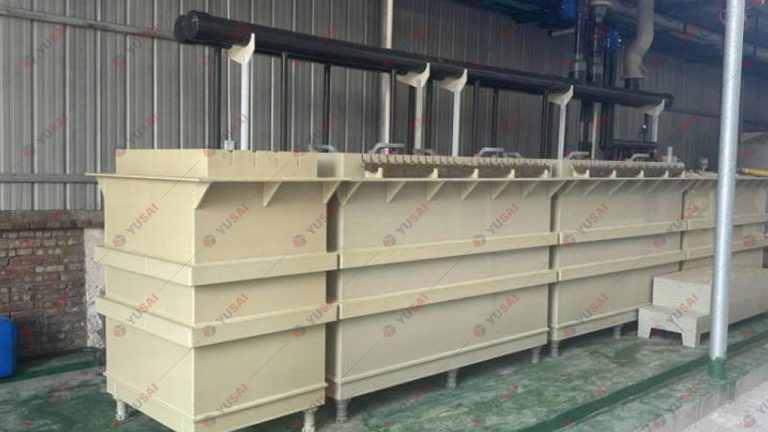
- Diaphragm Electrowinning for Au-Ag Alloy Deposition Thiourea pregnant solution is fed into cathode compartment of diaphragm electrolyzer equipped with cation exchange membrane. Acidic solution (sulfuric acid or sulfuric-nitric mixed acid, pH=0.5–1.5) fills the anode compartment. Titanium plate serves as cathode; 1 wt% Ag lead-silver alloy plate works as anode. Electrolyte temperature:30–50 ℃, cathode current density:5–50 A/m², electrowinning time:10–15 h. Gold and silver are simultaneously reduced and deposited on titanium cathode surface to form gold-silver alloy.
After electrowinning, spent catholyte passes through ion exchange resin to adsorb residual trace gold and silver. The treated liquor is re-adjusted to target thiourea concentration and recycled back to thiourea leaching tank to reduce reagent consumption.
Key Advantages
✅ High precious metal recovery performance Gold leaching >95%, silver leaching >99%; electrowinning deposition efficiency Au>99.5%, Ag>98.5%. Direct recovery Au>94%, Ag>96%.
✅ Selective leaching, valuable elements separated naturally Under acidic thiourea condition, gold and silver are selectively dissolved while selenium and tellurium remain in solid residue. It enables separate recovery of precious metals and rare metals without complicated impurity removal steps.
✅ Full hydrometallurgy, low environmental impact No smelting furnace, no toxic flue gas and heavy metal dust. Operates at atmospheric pressure and mild temperature; low energy consumption and lower investment compared with pyrometallurgy.
✅ Reagent recycling & lower operation cost Thiourea bearing tail liquor is recovered by ion exchange, re-formulated and reused in leaching stage. Copper sulfate lixivium returns to copper refinery, maximizing resource utilization.
✅ Mild operating condition & simple equipment No high-pressure autoclave required. Atmospheric leaching reduces equipment investment and safety risks for small & medium metal recycling plants.
Comparative Edge vs Existing Technologies
Conventional pyrometallurgical anode slime treatment relies on smelting and has severe lead/arsenic fume hazards, long workflows and high energy cost. Other hydrometallurgical routes use aqua regia, nitric acid or high-pressure thiocyanate leaching, which bring strong corrosivity, complex multi-step purification, large dosage of ammonia and hydrazine hydrate and extra refining work for final gold/silver powder.
Our thiourea leaching + diaphragm electrowinning method avoids high-pressure reactor, reduces impurity interference, and directly produces gold-silver alloy at cathode, shortening production chain.
Application Scenarios
- Copper smelter anode slime precious metal recovery
- Secondary non-ferrous metal recycling plant
- Small & medium-scale precious metal refineries
- Comprehensive recovery project for copper, gold, silver, selenium and tellurium from copper refining by-products
Summary
This full wet metallurgical process realizes selective extraction of gold and silver from copper anode slime by sulfuric acid decoppering, thiourea leaching and diaphragm electrowinning. It delivers high Au & Ag recovery rate, separates selenium and tellurium into residue for further extraction, adopts liquor circulation to cut reagent cost, and greatly reduces pollutant emission. It is an eco-friendly and economical technical solution for copper anode slime precious metal recycling.