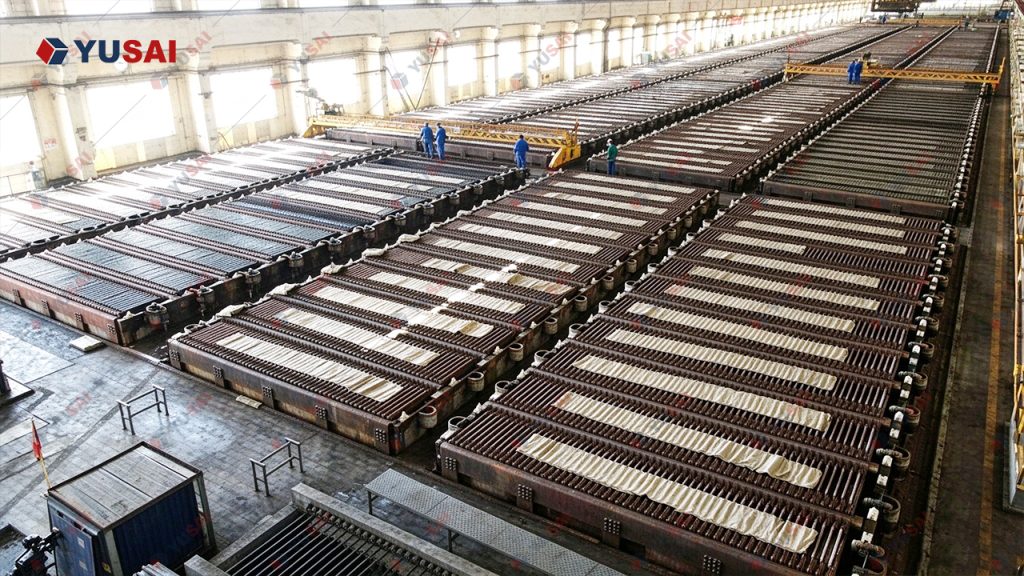
Aluminum reduction pots are the core assets in primary aluminum smelting. Consistent, well-controlled daily maintenance helps extend pot service life, lower specific energy consumption, reduce unplanned outages and support stable, incident-free production. Typical pot tending activities include carbon slag removal, electrolyte level adjustment, pot side crust profiling, manual fixture retorquing, electrolyte tapping and electrolyte feeding. Proper standardized work procedures significantly mitigate common risks such as thermal burns, scalds, electric shock, impact injuries, slips, falls and pinch injuries.
1. Carbon Slag Removal
Carbon slag builds up on the electrolyte surface and disturbs current distribution and internal thermal balance of the pot, so periodic removal is required. Preparation: Gather required tools: chisels, slag skimming shovels and multi-tooth rakes. Confirm the target pot identifier and remove local pot cover panels. Preheat all ferrous tools before entering the hot zone.
Operating Procedure: Activate the tapping crust breaker to open the tapping outlet. For slag removal at corner or side crust zones, coordinate with the overhead crane for crust breaking. Hook out crust lumps and rest them on both sides of the opening. Insert the slag shovel into the center seam or side seam, skim steadily from inside outward along the electrolyte surface to collect carbon slag near the tapping outlet, then transfer slag into the slag bin. Once complete, rebuild the crust, clean the work zone, reinstall pot covers and return all tools to storage.
Critical Notes: If heavy carbon slag is observed during anode change-out, complete slag removal before installing new anode assemblies. Take care to minimize electrolyte carry-over while skimming slag.
Job Record: Document the pot ID and work location in the site work log.
2. Pot Side Crust Profiling
Side crust profiling manages thermal insulation and heat dissipation of the reduction pot, stabilizes the frozen ledge profile and prevents localized overheating and anode oxidation. Preparation: Prepare shovels, aluminum rakes, chisels and brooms. Confirm the target pot and working side. Remove a maximum of six cover panels at one time. Uncover and replace panels sequentially; never expose a large pot side area all at once.
Operating Procedure: Verify insulation covering thickness: 15–18 cm over standard anode areas, 18–20 cm for corner anodes. Add or remove covering material and level the surface. Clear accumulated alumina under crust breakers and feeders; redistribute excess alumina to areas with thin insulation and log feeder blockages for prompt maintenance. Inspect anodes and recover any exposed anode surfaces to stop oxidation. Seal and profile any open fire cracks immediately. Remove oversize old crust blocks using chisels or crane support and replenish insulation material. Maintain side heat dissipation channel width at 6–8 cm (excluding corner anode zones weighted with hold-down iron for enhanced insulation). Rectify side or center seam collapse, oversized lumps and low covering material. Upon completion, clean the area, refit covers and stow all tools.
Quality Acceptance Criteria: Insulation thickness meets specification. Crust fragments along side and center seams ≤5 cm. Cover surface is level with natural side slopes, no open gaps, no exposed or oxidizing anodes, to maintain balanced heat retention and heat loss.
Job Record: Enter pot ID and profiled section in the work log.
3. Electrolyte Level Adjustment (Electrolyte Tapping & Feeding)
Electrolyte level directly affects pot voltage, ledge stability and overall pot performance. Tapping and feeding operations must follow approved safe work practices. Preparation: Confirm target pot ID. Prepare large ladles, electrolyte bins, electrolyte transfer bags, chisels, steel punch bars, shovels, multi-tooth rakes and brooms. Fully preheat all ferrous tools.
Electrolyte Tapping: Use the crust breaker to open the tapping outlet and furnace door. Enlarge the opening with punch bars and chisels so the ladle can move freely. Remove crust blocks around the opening and place them on the crust. Position the electrolyte bin or transfer bag beside the tapping outlet. The operator stands on the opposite side, ladles electrolyte slowly and pours steadily into the container until the target volume is reached. Restore the tapping outlet crust, clean the work area, close the furnace door and return tools.
Electrolyte Feeding: Open the tapping outlet and furnace door with the crust breaker. Enlarge the opening to accommodate the transfer bag spout. Clear surrounding crust fragments. Move the filled electrolyte bag into position, align the spout with the tapping outlet and tilt the bag gradually to feed electrolyte into the pot. Stop feeding once the target electrolyte level is achieved. Rebuild the outlet crust, clean the zone, reinstall end covers and return all tools.
Critical Notes: Work slowly and keep the ladle facing upward to avoid drawing molten aluminum. Stop all tapping work immediately if an anode effect occurs.
Job Record: Record pot ID and electrolyte volume transferred in the work log.
4. General HSE Rules for All Pot-Top Work
All personnel must wear complete site PPE: safety helmet, flame-resistant coveralls, safety footwear, face shield, safety spectacles and heat-resistant gloves. Inspect all hand tools before use to confirm serviceable condition. Handle pot cover panels carefully. Do not stack panels where they could fall and cause injury; avoid removing excessive panels at once. Keep ferrous tools clear of busbars to prevent short circuits and electric shock hazards. Do not strike the crust with excessive force, which can eject high-temperature electrolyte. Follow overhead crane site safety procedures when working with cranes and inspect lifting gear before lifting. All metal tools inserted into the hot pot must be preheated to prevent steam explosion from residual moisture. Prohibited: Standing or walking directly on the hot pot crust. Before starting pot-top work, verify pot covers are securely seated and assign a dedicated spotter / attendant. At least two workers are required when adjusting cover plates with wrenches, with one acting as lookout. Manual fixture retorquing: the pot-top worker must wear a fall-arrest harness, stand only on designated footrests, anchor the lanyard to an adjacent fixture head and apply force evenly. Maintain adequate clearance when striking anode rods with sledgehammers to prevent flying hammer hazards. Ladles and electrolyte containers must be dry and preheated. Preheat slag bins by adding a small test volume of electrolyte first before continuous pouring to avoid flash steam explosion. Before transfer, sprinkle alumina across the liquid electrolyte surface to form a thin solid crust. Move containers slowly and smoothly to prevent splashing. When lifting electrolyte bins by overhead crane, maintain lift height below 0.5 m above floor level. Ground personnel must keep a minimum 2 m safe distance. Do not reposition bins until electrolyte inside has fully solidified. Rotate crew regularly during high-heat slagging and electrolyte transfer tasks to prevent heat stress and PPE damage. Cease all pot-top activities immediately during an anode effect to reduce electrical risk. Never throw tools from the pot top or jump down from the pot deck. Install warning signage before cleaning underneath pots. Do not work directly beneath tapping outlets. Use only designated access walkways; do not climb through panels or window openings. Remove conductive debris bridging busbars immediately. Do not place carbon blocks or ferrous tools on busbars or bus support piers.
5. Summary
Structured, standardized daily maintenance of aluminum reduction pots stabilizes thermal balance, raises current efficiency, cuts power consumption and protects people and plant assets. All procedures are built around hot molten salt safety and primary aluminum smelting process requirements. We supply complementary pot-tending equipment including carbon slag skimming tools, electrolyte transfer containers and crust-breaking accessories engineered for heavy-duty smelter environments, fully compatible with this safe work system.