Abstract
The composition of the electrolyte directly affects the manganese electrowinning process. Removing impurities such as iron, cobalt, nickel, copper, zinc, lead, tin, and other heavy metals, as well as non-metallic elements and organic substances, can effectively improve electrolyte quality. High-quality electrolyte helps increase production capacity, reduce DC power consumption, and improve the economic efficiency of enterprises. Based on this, this paper discusses the optimization of the electrolyte purification process in electrolytic manganese metal production.
Keywords: electrolytic manganese metal; electrolyte; impurity removal; oxidative iron removal; manganese ore raw materials
1 Introduction
In electrolytic manganese metal production, the declining quality of manganese ore raw materials has made it difficult for conventional electrolytic processes to maintain stable electrolyte quality. This leads to poor stability of the electrolytic manganese bath, a continuous decrease in current efficiency, excessive consumption of manganese sulfate solution per unit of manganese product, and low manganese recovery. The low recovery of manganese from raw materials and low energy utilization are the main factors restricting the development of the electrolytic manganese industry. Therefore, it is necessary to reform the production process.
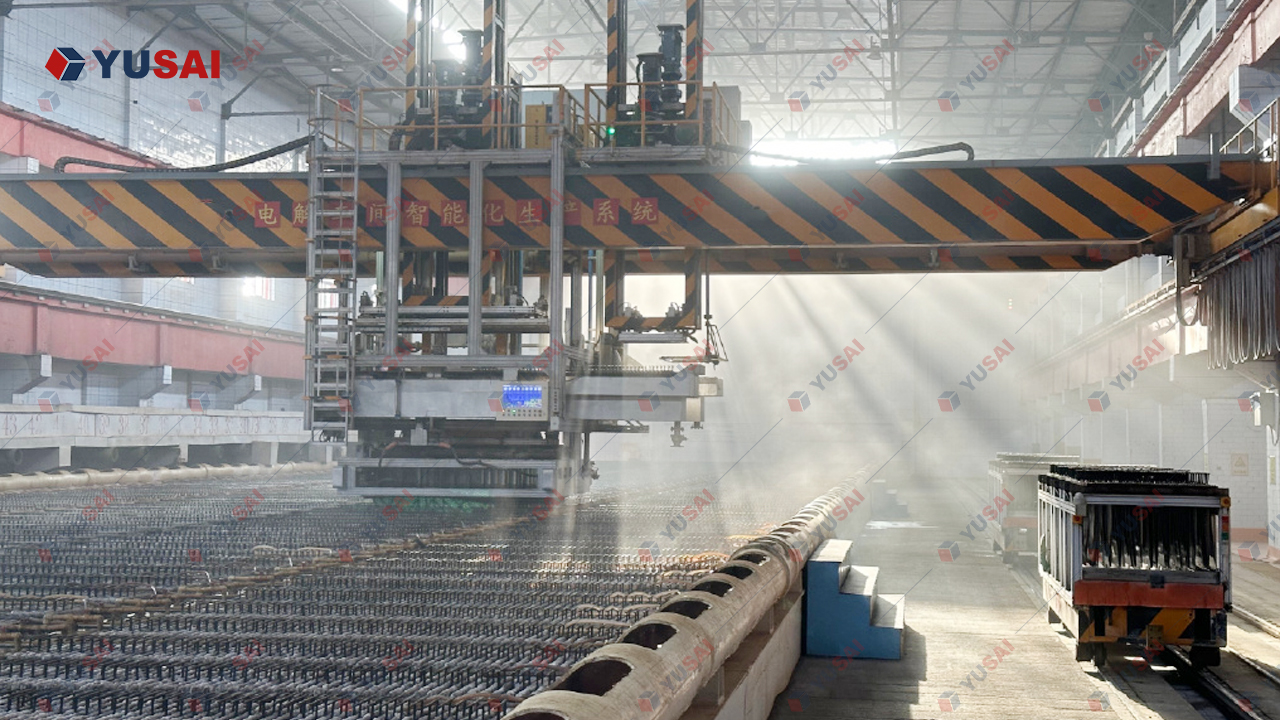
2 Impurities in Electrolytic Manganese Electrolyte
Heavy metals such as iron, copper, nickel, and cobalt have standard electrode potentials similar to those of manganese. During electrolysis, these metals may deposit on the cathode together with manganese and react with H⁺ to generate hydrogen. This reduces current efficiency, lowers manganese purity, and may result in unqualified products.
Impurities containing carbon, sulfur, and phosphorus can reduce selenite ions in selenium dioxide to elemental selenium, thereby weakening the effect of electrolytic additives. Excessive fluoride can reduce current efficiency and even cause corrosion of electrode plates, affecting the manganese electrodeposition process.
Arsenic is one of the most harmful impurities. When the arsenic concentration in the electrolyte reaches 0.05 g/L, current efficiency decreases rapidly, manganese deposition is inhibited, and black substances may form on the cathode, seriously affecting product quality. Therefore, reducing impurity levels in the electrolyte and improving manganese purity and product quality are important tasks for metallurgical researchers.
3 Experimental Study on Electrolyte Purification
3.1 Raw Materials and Reagents
The main raw materials and reagents used in the experiment include pure sulfuric acid, pure ammonia water, industrial-grade liquid SDD, and inorganic sulfiding agent A. The anolyte has a Mn ion concentration of 14.06 g/L and a sulfuric acid concentration of 28.59 g/L. The solid materials include industrial metallurgical manganese powder, manganese carbonate powder with Mn²⁺ content of 16.3%, and roasted manganese powder with Mn²⁺ content of 31%.
3.2 Experimental Equipment
The experimental equipment includes a thermostatic water bath, a 5000 mL beaker, a 3000 mL beaker, and an electric stirrer.
3.3 Experimental Methods
Comparative experiments were conducted using different iron removal sequences.
A certain amount of electrolytic manganese anolyte was placed in a 4000 mL beaker. The Mn²⁺ concentration of the leachate was controlled at 39 g/L, and 542.5 g of manganese carbonate powder was added. Sulfuric acid was then added at an acid-to-ore ratio of 0.53 for leaching. The leaching process lasted about 120 minutes at a water bath temperature of 55 °C. After leaching, samples were taken to analyze Fe²⁺ and H₂SO₄ content. The reacted solution was divided into four equal parts for parallel tests.
One group was added with roasted ore containing 14% manganese metal, the pH value was adjusted to about 3, and then a certain amount of metallurgical manganese powder was added for oxidative iron removal.
Another group followed the same procedure, but metallurgical manganese powder was added first, and then roasted manganese powder was added to reduce residual acid. The amount of metallurgical manganese powder was the same as the iron content, but the iron removal sequence was different.
In addition, two equal portions of leachate—one from full manganese carbonate ore and one from mixed manganese carbonate and roasted ore—were treated with the same amount of liquid SDD and a mixture of liquid SDD and inorganic sulfiding agent A, respectively. The changes in heavy metal concentrations were observed.
4 Results and Process Optimization
4.1 Comparison of Different Purification Methods
The experimental results show that after treatment with SDD and SDD combined with inorganic sulfiding agent A, the contents of cobalt, nickel, copper, lead, cadmium, and other harmful impurities in the leachate are basically equivalent and meet production requirements.
However, the zinc content in the manganese sulfate solution produced from manganese carbonate ore is more than twice that from roasted ore. SDD has a poor effect on zinc sulfidation, while inorganic sulfiding agent A has a significant zinc removal effect. When zinc in the electrolyte exceeds 3 mg/L, it will affect manganese deposition and easily cause bath alkalization and abnormal cathode deposition.
Therefore, while using SDD for impurity removal, inorganic sulfiding agent A should be added to remove zinc. Zinc ions can combine with sulfide ions to form stable zinc sulfide precipitates, thereby reducing zinc ion content in the electrolyte, improving electrolyte purification efficiency, reducing dependence on roasted ore, simplifying the production process, and reducing production costs.
4.2 Comparison of Different Iron Removal Sequences
Under the same dosage of metallurgical manganese powder, better iron removal effect can be obtained by adding metallurgical manganese powder first and then roasted manganese powder to neutralize residual acid.
Oxidative iron removal by manganese dioxide requires acidic conditions. Increasing H⁺ concentration promotes the forward reaction and improves the oxidation efficiency. When roasted ore is added for iron removal first, the pH value of the solution is about 3, while the optimum pH for iron oxidation by MnO₂ is below 1.5. Higher pH reduces the oxidation efficiency of the oxidizing ore and increases its consumption.
Therefore, adding a certain amount of metallurgical manganese powder before iron removal can effectively reduce the consumption of metallurgical manganese powder. According to the experimental results, this process can save about 110 yuan per ton of manganese product. For an annual output of 60,000 tons, about 8,200 tons of metallurgical manganese powder can be saved annually, equivalent to a cost reduction of about 6.6 million yuan.
5 Conclusion
Adding metallurgical manganese powder for oxidative iron removal before the manganese carbonate leaching reaction is completed, and then adding roasted manganese powder to reduce residual acid, can achieve better iron removal results. At the same time, the combined use of SDD and inorganic sulfiding agent A can effectively reduce zinc and lead contents and maintain stable solution quality.
The optimized process can alleviate the problems of low current efficiency and bath deterioration in the full-acid process, and provide technical support for process improvement, production cost reduction, and reduced dependence on roasted ore raw materials.