Copper electrorefining is the core process for high-purity cathode copper production. During electrolysis, precious metals including gold, silver, platinum and palladium remain undissolved and concentrate into copper anode slime, the most valuable by-product of copper smelters. The recovery rate, automation and environmental performance of precious metal extraction directly determine the overall profitability of smelting projects. We specialize in supplying complete sets of precious metal recovery equipment and integrated process solutions for copper refineries worldwide.
1. Source of Precious Metals: Anode Slime from Copper Electrolysis
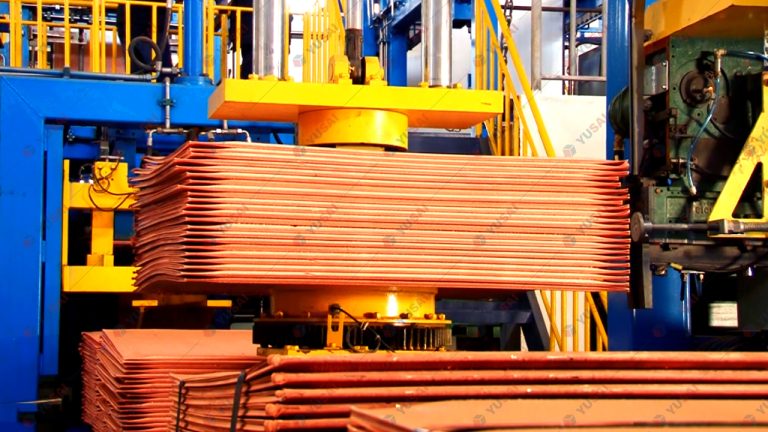
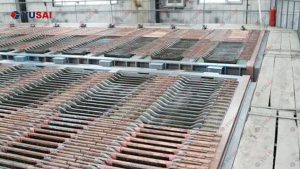
Inside copper electrolytic cells, copper anodes dissolve while pure copper deposits on cathodes to produce 99.99% cathode copper. Typical operating parameters: current density 230–280A/m², electrolyte temperature 58–65℃, sulfuric acid concentration 170–210g/L. Precious metals, selenium, tellurium, arsenic, antimony and bismuth do not dissolve and settle as anode slime. Modern smelters adopt high current density up to 320A/m², optimized busbar system and oxygen agitation, which changes the composition of anode slime. It puts higher requirements on anti-corrosion performance, selective separation and continuous operation of precious metal recovery equipment.
2. Global Technology Comparison for Precious Metal Recovery
Domestic Development in China
Major Chinese copper smelters (Jiangxi Copper, Tongling Nonferrous, Jinchuan, Daye Nonferrous) have expanded electrolysis capacity. Stainless steel cathodes account for 62% of total capacity. High current density electrolysis, oxygen stirring and intelligent short-circuit monitoring are widely applied, delivering stable anode slime output. Traditional pyrometallurgy is still mainstream, while short-process hydrometallurgy + electrorefining is rapidly tested:
- Oxygen agitation technology improves impurity sedimentation for easier precious metal separation;
- High-current-density test cells increase precious metal concentration in anode slime;
- Short-circuit detection systems reduce annual metal losses by hundreds of tons.
Main industry challenges: low localization rate of automation systems, high waste residue treatment cost, difficult removal of arsenic, antimony and bismuth impurities, limiting precious metal direct recovery.
Advanced International Routes
- North America: KIDD process & Kennecott smelter adopt high-efficiency electrolysis with titanium mother plates and automatic stripping lines. Anode slime collection is highly automated with low labor cost, yet the capital investment is high.
- Europe: Norddeutsche Affinerie and Outokumpu develop advanced electrolyte purification to remove As, Sb, Bi simultaneously, reducing impurity load for precious metal refining. Pulse power technology refines cathode grains and cuts precious metal entrainment loss, with strict wastewater discharge control.
Overseas refineries widely use closed anode slime collection, continuous leaching and automatic precious metal electrorefining lines for stable recovery and full environmental closed-loop management.
3. Iteration of Core Precious Metal Recovery Equipment
Our modular complete equipment covers the whole workflow: anode slime pretreatment, leaching, solid-liquid separation, Au/Ag/Pt/Pd electrorefining and harmless residue treatment.
- Full plastic anti-corrosion reaction tanks & closed leaching system: strong acid resistance, long service life, minimize flue gas emission and precious metal loss.
- Precious metal electrorefining units: stepwise electrowinning for gold, silver, platinum and palladium, final purity up to 99.99%, equipped with durable titanium electrodes.
- Intelligent solid-liquid separation & automatic anode slime collector: online slime collection connected to copper electrolysis workshop, less manual operation and higher metal recovery.
- PLC automation & online monitoring module: real-time control of temperature, acidity and metal ion concentration, saving chemical consumption and metal loss.
- Residue harmless treatment unit: separate hazardous As/Sb/Bi, cut hazardous waste cost and meet global environmental standards.
Digital twin, online elemental analyzers and waste heat recovery are new industry trends to realize remote inspection and adaptive parameter control.
4. Project Reference: Supporting Precious Metal Recovery for Copper Refineries
For a 350,000 tpy cathode copper project, our precious metal recovery plant processes copper anode slime to extract gold and silver efficiently. The system can connect to existing copper electrolysis lines without massive reconstruction. We optimize impurity removal to reduce steam and reagent consumption and lift overall precious metal recovery. Modular design supports pilot scale to large smelter projects with flexible capacity expansion.
5. Industry Challenges & Our Technical Advantages
Common global pain points:
- Fluctuating anode slime composition leads to precious metal entrainment loss;
- High cost of imported titanium electrodes and online elemental analyzers;
- High hazardous waste disposal cost and strict environmental compliance.
Our equipment solutions solve these issues:
- Custom pretreatment & selective leaching units to separate arsenic, antimony and bismuth while protecting precious metals;
- Localized anti-corrosion electrolytic cells & electrode assemblies to lower CAPEX and OPEX;
- Fully closed process with recycled wastewater, hazardous waste reduction, complying with regulations in Europe, Southeast Asia and Middle East;
- Modular layout for phased construction, suitable for greenfield projects and old plant revamping.
6. Future Trends & Cooperation
Global copper electrolysis develops toward ultra-high current density, intelligence and low carbon. The resource value of anode slime keeps rising. Digital twin, new membrane materials and waste heat recovery will further reduce energy consumption for precious metal recovery.
We deliver full services: lab test, complete equipment manufacturing, site installation, commissioning and operator training. We provide customized precious metal recovery packages for copper smelters and secondary copper refineries worldwide. Whether for new copper electrolysis projects or plant modernization, we select equipment and design process flows according to anode slime composition and capacity targets, helping customers maximize precious metal revenue from anode slime.
Keywords: copper anode slime precious metal recovery, gold silver platinum palladium refining equipment, copper smelter precious metal recovery plant, anode slime processing system